A reducing agent can determine whether a metal surface meets specification, a wastewater stream can be discharged safely, or a sensitive manufacturing reaction remains under control. The industrial uses of reducing agents extend well beyond a single process step: they are applied to remove oxygen, convert metal ions, neutralize residual oxidizers, preserve product quality, and support analytical testing. For procurement and operations teams, selecting the correct reducing agent is therefore a decision about process consistency, safety, and supply continuity.
Reducing agents work by donating electrons to another substance. In practical terms, this causes the other substance to be reduced while the reducing agent is oxidized. The chemistry is straightforward in principle, but the right product depends on the reaction target, operating pH, required purity, contact time, downstream treatment requirements, and equipment compatibility.
Where Reducing Agents Are Used in Industry
Metal finishing and surface treatment
Metal finishing is one of the most established applications for reducing chemistry. Reducing agents can convert dissolved metal ions into a lower oxidation state, recover metals from process solutions, or support electroless plating systems. Sodium hypophosphite, for example, is widely associated with electroless nickel plating, where controlled reduction deposits nickel on a prepared surface without an external electrical current.
In pickling, stripping, and conversion processes, reducing compounds may also help manage oxidation on metal surfaces or adjust bath chemistry. The choice of product must match the alloy, bath composition, operating temperature, and finish requirement. A chemical that performs well on carbon steel may not be appropriate for aluminum, copper, or stainless steel.
For metal processors, consistency matters as much as reaction performance. Variation in concentration, impurities, or moisture content can affect deposit quality, bath life, and reject rates. Clear labeling, batch traceability, and fit-for-purpose grades help maintain repeatable production conditions.
Water and wastewater treatment
Many water treatment systems use reducing agents to remove residual oxidizers before discharge or before water enters a downstream process. Sodium bisulfite, sodium metabisulfite, and sodium thiosulfate are commonly used to dechlorinate water after chlorination. In applications involving chlorine dioxide, chloramines, peroxide, ozone, or other oxidizing disinfectants, the reducing agent must be chosen for the oxidant present and the required reaction speed.
Dechlorination is not simply a matter of adding enough chemical to achieve a test result. Overdosing can increase dissolved solids, alter pH, consume oxygen in receiving waters, or create an unnecessary chemical load for downstream treatment. Underdosing can leave harmful oxidant residuals. Reliable dosing requires validated calculations, suitable metering equipment, representative monitoring, and an understanding of process variability.
Reducing agents may also be used in wastewater streams containing hexavalent chromium. Chromium(VI) is reduced to chromium(III), which can then be precipitated and removed under controlled treatment conditions. This is a critical application where chemical selection, pH control, reaction verification, and sludge management must be addressed together.
Electronics and precision manufacturing
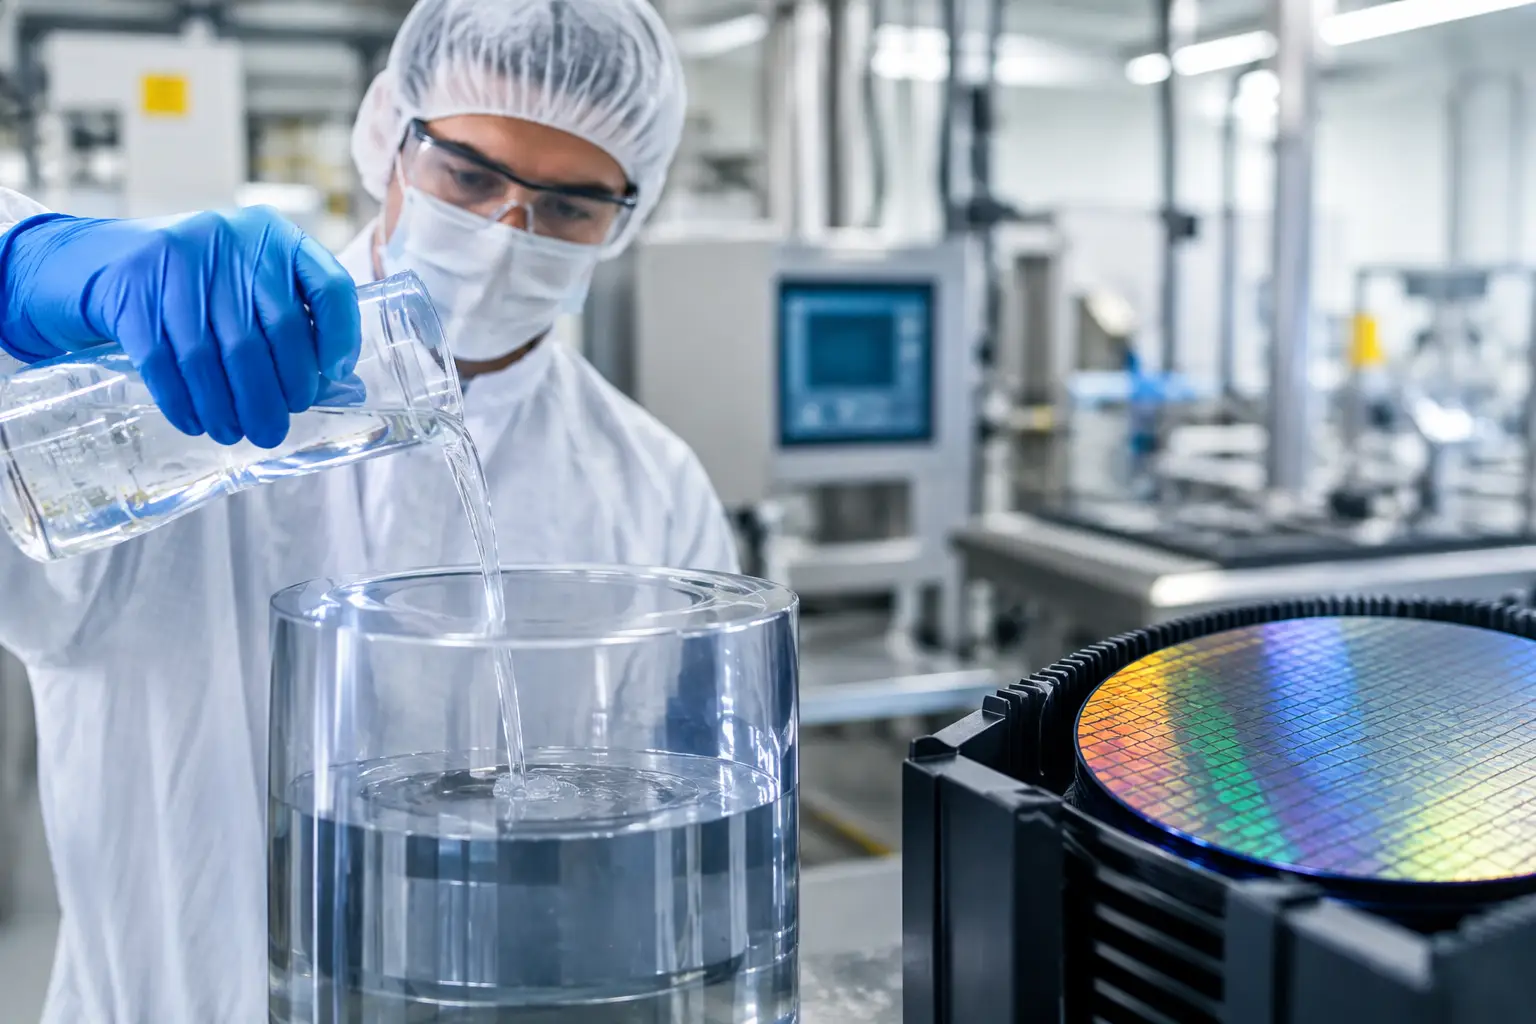
In electronics, wafer processing, and precision cleaning, oxidation control can affect yield and reliability. Reducing agents may be used in specialized cleaning solutions, metal deposition processes, and chemical formulations where surface condition must be tightly controlled. Here, the grade of chemical is often as important as the chemical identity.
Trace metals, particulates, and other contaminants that may be acceptable in general industrial material can cause issues in high-sensitivity applications. Laboratory reagent, analytical, ACS, or other specified grades may be required depending on the process and customer specifications. Procurement teams should avoid assuming that a higher-grade product is automatically the best choice, however. The correct grade is the one that meets contamination limits and process requirements without adding avoidable cost.
Chemical processing and manufacturing
Reducing agents are used across chemical manufacturing to control reaction pathways, prepare intermediates, and stabilize formulations. Sodium dithionite, for instance, is used as a reducing and bleaching agent in selected textile, pulp, paper, and chemical-processing applications. Formic acid, hydrazine derivatives, sulfites, and metal powders may also serve reducing functions in specific systems.
The trade-off is that reducing agents can introduce byproducts, salts, gases, or heat. Sulfite-based materials may generate sulfur dioxide under acidic conditions. Certain reactive reducing agents can decompose with heat or moisture. Others may react strongly with oxidizers. Process teams should assess the complete reaction system rather than evaluating a material only by its active content or purchase price.
Food, textile, pulp, and bleaching processes
Some reducing agents support bleaching, color correction, oxygen removal, and preservation-related processes. Their use is governed by sector-specific requirements, product-contact considerations, and local regulations. In food-related operations, only materials suitable for the intended application should be considered, with appropriate documentation and controlled handling.
Textile and pulp operations often balance bleaching performance against fiber quality, wastewater impact, and process economics. A faster or stronger reducing agent is not always preferable if it creates excess chemical demand, compromises material properties, or complicates effluent treatment. Trial work under actual operating conditions is often the most dependable route to selection.
Selecting the Right Reducing Agent for the Job
A practical selection process starts with the oxidizing species or metal ion that must be treated. The reaction must be effective at the actual process pH, temperature, concentration, and residence time. Compatibility with tanks, pumps, seals, and dosing equipment should be confirmed before implementation.
The following factors usually shape a sound purchasing decision:
- Required chemical grade and impurity limits
- Active content, physical form, and solubility
- Packaging suited to consumption rate, from laboratory bottles to drums or bulk supply
- Storage life and sensitivity to heat, air, moisture, or contamination
- Hazard classification, handling controls, and waste-treatment implications
- Batch documentation and supply reliability for planned production volumes
These points are connected. A powder may offer favorable transport economics but require dust control and careful dissolution. A liquid product may simplify dosing but involve more frequent deliveries or higher freight weight. A concentrated material can reduce storage demand, yet may require more rigorous handling controls. The best option is the one that supports the entire operation safely and predictably.
Storage, Handling, and Quality Control
Reducing agents should be segregated from incompatible oxidizing materials and stored according to the product safety data sheet. Many materials require dry, cool storage in tightly closed containers to limit degradation. Sulfite-based chemicals, for example, can lose effectiveness when exposed to air or moisture, while some products create hazardous gases if mixed with acids.
Good chemical management also depends on receiving inspection, legible container labels, stock rotation, and documented batch records. For operations that rely on concentration-sensitive reactions, incoming checks may include appearance, assay, pH, specific gravity, or application-based verification. Laboratory teams can use appropriate reagent grades for method development and quality-control testing, then align production material specifications with proven process needs.
Personnel should have access to suitable personal protective equipment, spill-response procedures, and clear instructions for dilution and transfer. Never treat reducing agents as interchangeable simply because they serve a similar purpose. Their reaction rates, hazards, residuals, and storage requirements can differ substantially.
A Supply Strategy That Supports Production
Chemical availability becomes a production issue when a treatment system, plating line, or manufacturing batch depends on a specific reducing agent. Buyers should consider not only unit price but also lead times, packaging availability, supplier stock planning, technical documentation, and the ability to maintain consistent specifications over repeat orders.
For Malaysian organizations managing industrial, laboratory, and treatment operations, Chemedic can help assess product fit by application, grade, packaging, and handling requirements. Its ISO 9001:2015-certified processes, traceability practices, and established distribution capability support customers who need a dependable chemical supply relationship rather than a one-time transaction.
A reducing agent should be selected as part of a controlled process, not as a commodity chosen in isolation. When chemistry, quality requirements, handling practices, and delivery planning are aligned, the product can do its intended work without becoming the source of the next operational problem.