A waste container becomes a serious operational problem long before it leaves the site. When incompatible residues enter the same bottle, drum, or collection area, chemical waste segregation can determine whether a routine disposal task remains controlled or becomes a release, fire, pressure buildup, or exposure incident. For laboratories, production plants, and facilities teams, segregation is not simply an environmental housekeeping requirement. It is a core part of chemical control, traceability, and business continuity.
The most reliable programs begin before waste is generated. They connect purchasing, labeling, storage, use, collection, and disposal into one documented process. That approach gives staff clear instructions at the point of use while giving managers the information needed to select approved disposal routes and demonstrate proper control.
Why Chemical Waste Segregation Requires More Than Labels
A label that says “chemical waste” is not enough to establish compatibility. Waste composition can change through dilution, contamination, reaction byproducts, cleaning residues, and mixed-process inputs. A spent solvent may contain metals. An acidic rinse may contain oxidizers. A container of laboratory waste may include several materials that were compatible in a small experiment but are unsuitable for bulk accumulation.
The principal risk is incompatibility. Acids mixed with cyanide- or sulfide-containing waste can produce highly toxic gases. Acids and bases can generate significant heat and splashing. Oxidizers can intensify combustion when combined with organic solvents, oils, paper, or reducing agents. Certain metals or reactive materials may release flammable hydrogen in contact with water or acid.
Compatibility is not the only concern. Segregation also supports accurate waste classification, safer transport, contractor acceptance, and cost control. A container with a well-defined composition can usually follow a more predictable disposal pathway. A mixed, unknown, or poorly documented container may require additional assessment and specialized handling.
Start With a Practical Waste Inventory
Effective segregation starts with an inventory of the chemicals and processes that produce waste. This should include routine operations as well as maintenance activities, laboratory trials, cleaning, spill response, and seasonal production changes. Review safety data sheets, process records, product labels, and prior disposal documentation to identify likely constituents.
For each waste stream, record the source, expected chemical components, physical state, approximate volume, concentration range, hazards, and container type. A usable description is specific enough for personnel and waste contractors to understand what is present. “Spent acetone from equipment cleaning, potentially containing resin residue” is more useful than “solvent waste.”
This exercise often exposes avoidable mixing. For example, a facility may be placing non-halogenated solvents, halogenated solvents, and aqueous cleaners into one drum because they originate in the same work area. Separating them at source can improve safety and may reduce treatment complexity.
Use Compatibility Groups, Not Just Department Names
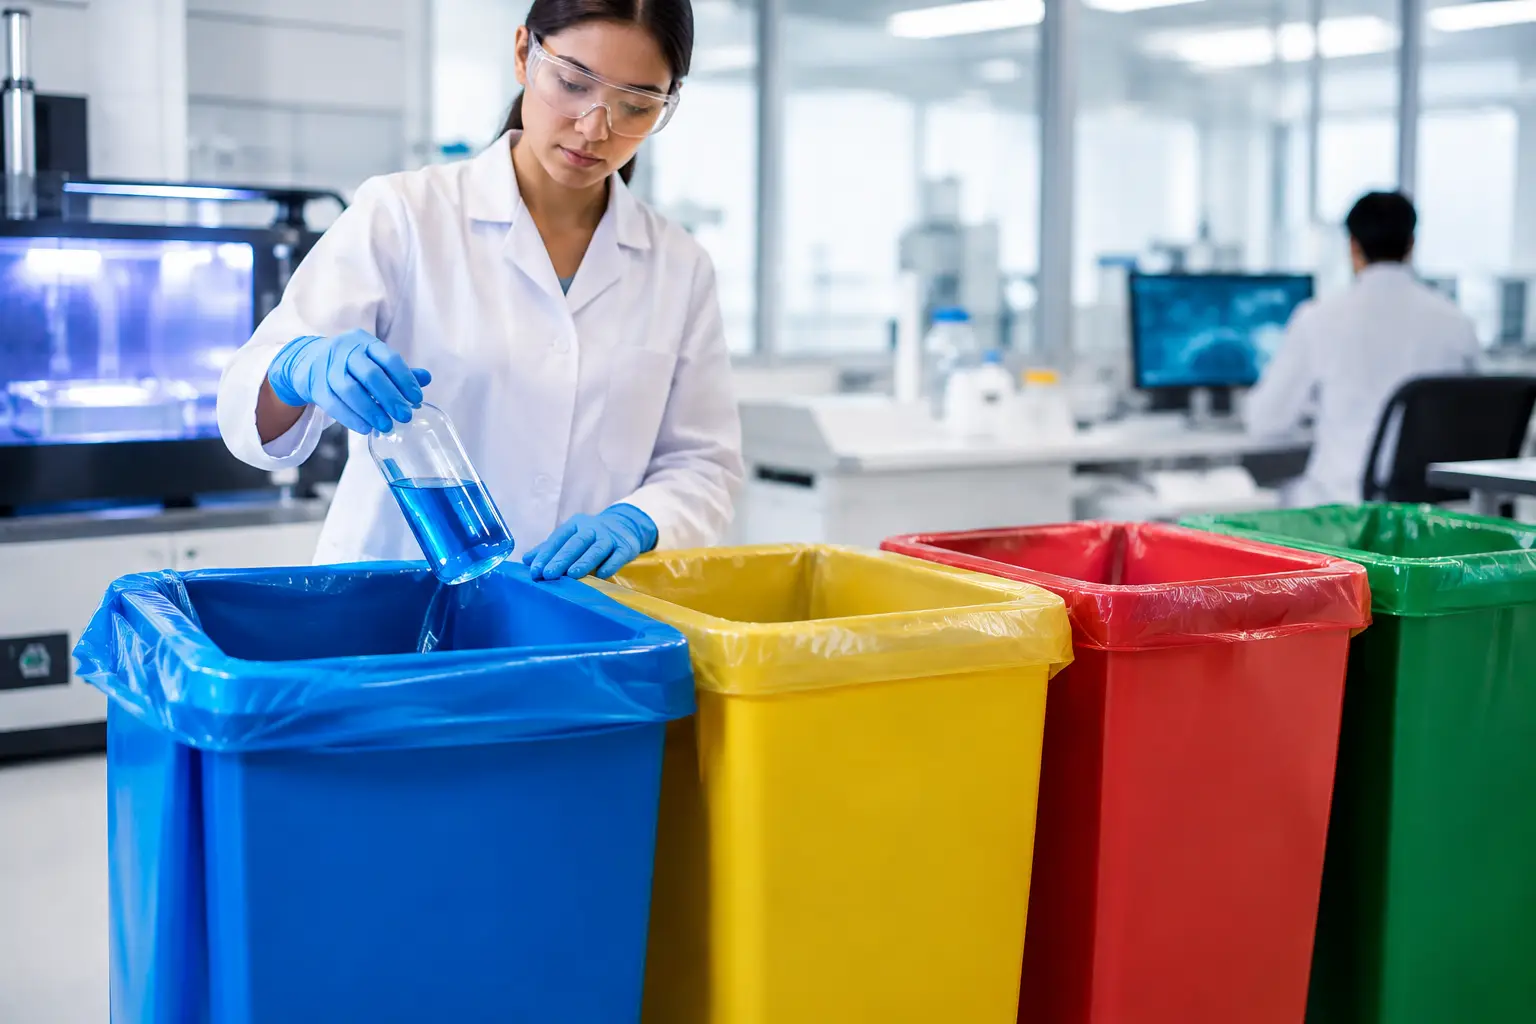
Waste should be grouped by chemical compatibility and hazard characteristics rather than by the department that generated it. The precise categories depend on the site’s materials, local regulatory requirements, and disposal provider’s acceptance criteria. However, a typical program distinguishes among:
- Acids and acidic metal-bearing solutions
- Alkalis and caustic cleaning solutions
- Halogenated and non-halogenated organic solvents
- Oxidizers, including concentrated oxidizing acids
- Reducing agents, sulfides, cyanides, and other reactive wastes
- Heavy-metal-containing residues, sludges, and solutions
- Oils, fuels, lubricants, and oily absorbents
- Contaminated solids, such as wipes, gloves, filters, and packaging
These categories should not be treated as universal mixing instructions. Two acid wastes, for example, may still require separation because one contains an oxidizer, fluoride, chromium compound, or dissolved metal that changes its hazard profile. The site’s written compatibility matrix should be based on the actual chemicals in use.
Control the Waste Stream at the Point of Generation
The point of generation is where most segregation failures begin. A central waste area may be well organized, but it cannot correct an unidentified or incompatible mixture that has already been created in a laboratory hood, plating line, maintenance bay, or janitorial store.
Provide designated, compatible containers where waste is generated. Each container should display a clear waste-stream name, applicable hazard warnings, accumulation start information where required, and enough space to identify the contents as they are added. Avoid relying on abbreviations that are understood only by one shift or department.
Containers must also be suitable for the material. Some solvents can attack certain plastics; hydrofluoric acid requires specialized compatible packaging; corrosive liquids may require secondary containment. Keep containers closed except when adding waste, do not overfill them, and inspect closures, labels, and exterior surfaces routinely.
A simple rule improves decision-making: if an employee cannot identify the correct container with confidence, they should stop and ask before adding material. Guessing to avoid a small delay creates a far larger problem later.
Design the Storage Area for Containment and Access
A properly designed central accumulation area provides physical separation as well as administrative control. Store incompatible groups apart, using separate cabinets, bays, trays, or secondary containment as appropriate to the quantities and hazards involved. Secondary containment should be compatible with the stored chemicals and sized to contain a foreseeable leak, not selected only for convenience.
Keep oxidizers away from flammables and organic materials. Separate acids from bases, and isolate materials that react with water or release toxic gases when exposed to acids. Maintain clear access for inspections and emergency response. Waste containers should never block exits, eyewash stations, electrical panels, or access routes.
Ventilation needs careful consideration. Some wastes may emit vapors, but indiscriminate venting can increase exposure or create other risks. Use containers and storage arrangements appropriate to the material, and follow technical guidance for substances that can build pressure or require specialized vented closures.
Make Traceability Part of Chemical Waste Segregation
Traceability protects both safety and disposal compliance. Every container should be traceable to a known source, process, and responsible area. This does not need to become an administrative burden. A practical log can capture the container ID, waste category, location, contents, date opened, responsible person or department, and collection date.
Batch traceability is especially valuable in laboratories, electronics production, metal finishing, water treatment, and food-processing environments where process chemistry changes over time. If a contractor questions a waste profile or an inspection identifies an inconsistency, records allow the site to investigate quickly rather than treating every container as unknown.
Procurement also has a role. When new chemicals, formulations, or cleaning products are introduced, the change review should consider the resulting waste stream. A product may meet process requirements while creating disposal challenges that were not present with the previous material. Product selection, packaging size, and available storage capacity should be assessed together.
Train for Decisions, Not Memorization
Training should focus on the decisions employees make during normal work: which container to use, what information to record, when a container is full, how to recognize damaged packaging, and who to contact when the waste does not match an established stream. Generic annual training has limited value if labels and work instructions at the point of use are unclear.
Use examples drawn from real site activities. A laboratory team may need guidance on separating solvent rinses from aqueous acid digests. A maintenance crew may need to distinguish used oil, oily rags, aerosol cans, and leftover cleaning chemicals. Production operators may need a clear escalation process when a batch is off specification.
Periodic inspections should reinforce the program rather than merely identify faults. Review labels, container condition, fill levels, segregation distances, logs, and housekeeping. When a recurring error appears, improve the system: relocate containers, revise labels, adjust collection frequency, or clarify the work instruction.
Balance Segregation With Operational Reality
Over-segregation can create too many small containers, increase handling, and make collection inefficient. Under-segregation creates incompatible mixtures and reduces disposal options. The right balance depends on chemical volume, composition variability, available storage space, site capabilities, and the requirements of the authorized waste management provider.
For low-volume laboratories, maintaining several clearly labeled small containers may be the safest choice. For higher-volume industrial operations, dedicated bulk containers with controlled transfer procedures may be more practical. In both cases, the process should be reviewed whenever production volume, chemical inputs, or disposal arrangements change.
Chemedic supports organizations that need to align chemical selection, labeling, packaging, and handling practices with their day-to-day operations. Reliable chemical management does not end when a product is used. It continues through the final documented handoff of the waste stream.
A well-run segregation program gives people a clear answer before they open a container: what this waste is, where it belongs, what it must never contact, and who is accountable for the next step. That clarity is one of the most practical safeguards any chemical-using operation can build.